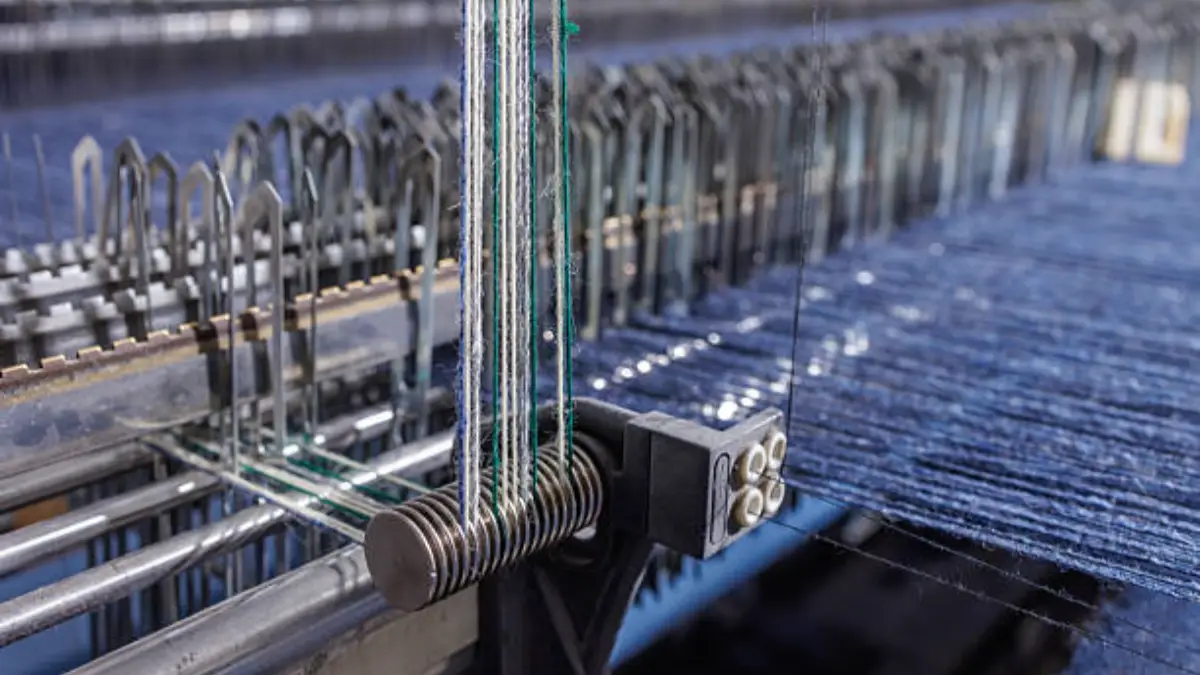
The denim dyeing process directly affects the color consistency, fading patterns, and quality of finished デニムジーンズ. A mismatch between product requirements and a manufacturer’s dyeing method can lead to shade variations and inconsistent colorfastness, affecting product quality and production costs.
This guide helps denim brands and apparel buyers evaluate suppliers by comparing rope and slasher dyeing, including their effects on ring-dye characteristics and fading potential. It also covers key quality control measures, from shade consistency to colorfastness testing, to help buyers set clear standards and maintain consistent results across production batches.
Denim Dyeing Process From Yarn Preparation to Finished Jeans
Making jeans is a two-part journey. First, cotton yarn is dyed and woven into denim fabric. Second, that fabric is cut, sewn, and put through extensive washing and finishing.
| 段階 1: From Yarn to Fabric | 段階 2: From Fabric to Jeans |
|---|---|
|
|
段階 1: From Yarn Preparation to Woven Fabric
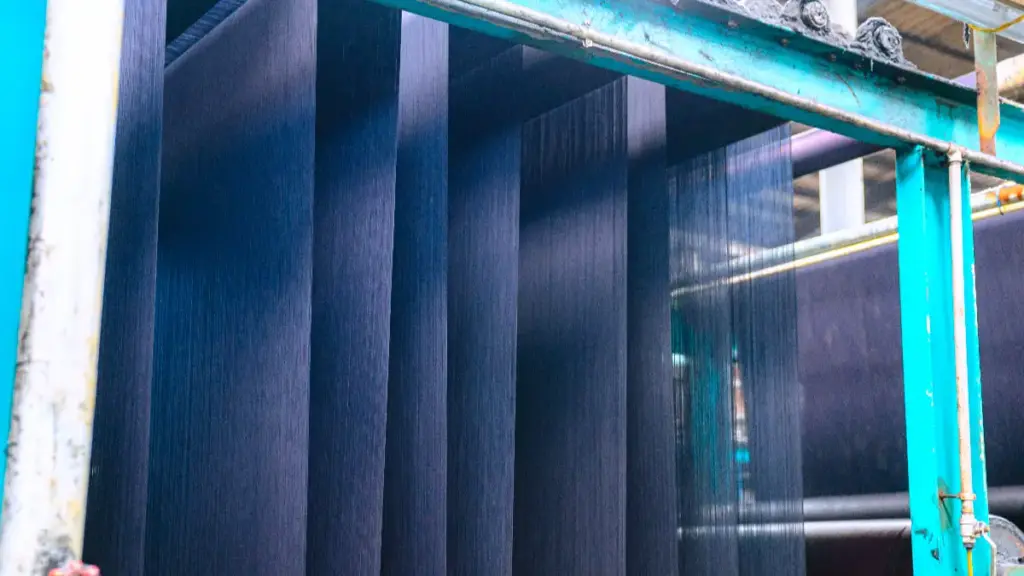
The first half of the process is all about creating the core material: the denim fabric itself. It begins with spinning cotton into strong warp yarns. These yarns are then assembled for dyeing. The two main industrial methods are rope dyeing and slasher (or sheet) 染色. Rope dyeing, where yarns are bundled into thick “ropes,” is considered the premium method for achieving high-contrast fades. スラッシャー染め, where yarns are laid out in a flat sheet, is more efficient for high-volume production.
Regardless of the method, the warp yarns are repeatedly dipped in indigo vats and exposed to air. This cycle builds color on the yarn’s surface, creating the “ring-dyed” effect—a dark outer layer with a white core—that is essential for how denim fades. After dyeing, a protective starch-based coating called sizing is applied. ついに, the indigo-dyed warp yarns are woven with undyed weft yarns, typically in a 3/1 twill pattern, to produce rolls of loom-state or “生” デニム生地.
段階 2: From Woven Fabric to Finished Jeans
This phase transforms the stiff, dark fabric into the finished jeans you see in a store. First, the fabric rolls go through finishing processes like desizing to remove the starch and sanforizing to control future shrinkage. After inspection, the fabric is cut into panels and sewn together into what are known as “生” または “硬い” ジーンズ.
The real transformation happens in the laundry. These raw jeans undergo extensive wet and dry processing to achieve the desired look, 感じる, そしてフィットします. Wet processing happens in large industrial washers and includes enzyme or stone washing to create an overall faded and softened effect, and sometimes bleaching for lighter shades. Dry processes create localized wear patterns like whiskers on the hips or faded areas on the knees. These are done by hand-sanding, specialized machinery, or increasingly, レーザー. After all the washing and finishing, the jeans are dried, inspected one last time, and prepared for shipment.
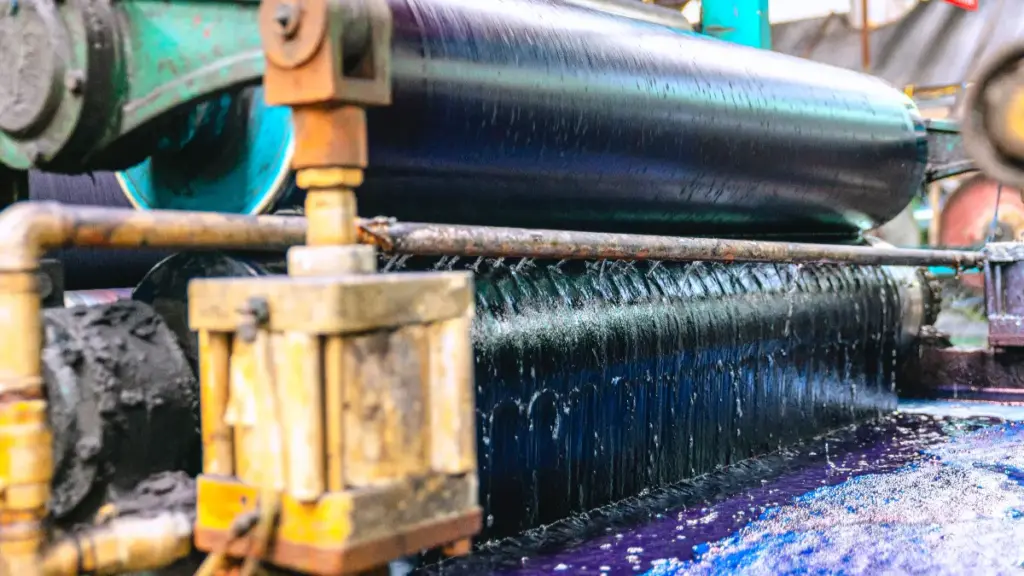
Indigo Dyeing Methods Used in Modern Denim Manufacturing
Rope dyeing creates high-contrast fades for premium denim, while slasher dyeing provides high-speed, cost-effective production for the mass market. This choice defines the denim’s final character.
Rope Dyeing for Premium and Heritage Denim
Rope dyeing is widely used for premium and heritage denim. Manufacturers gather warp yarns into thick ropes and pass them through multiple indigo dye baths. 浸すたびに, the yarns undergo air exposure, known as skying, which allows the indigo to oxidize. Manufacturers repeat this cycle, often 6–12 times, to achieve the desired shade. After dyeing, they dry the yarns, re-beam them into a flat sheet, and apply sizing separately.
This process creates a strong ring-dye effect, with indigo concentrated near the yarn surface and a relatively white core. As washing and abrasion remove the outer blue layer, the white core becomes visible, creating the high-contrast fades associated with heritage denim.
- Market Position: プレミアム, 耳, and heritage denim that requires distinctive fading.
- Cost and Complexity: Requires additional steps, including ball warping and re-beaming, increasing production costs.
- Shade Consistency: Helps maintain consistent color along yarn lengths, although manufacturers must control variations between ropes.
Slasher Dyeing for Mass-Market and Fashion Denim
スラッシャー染め, also called sheet dyeing, prioritizes speed and cost efficiency. Manufacturers spread warp yarns into a flat sheet and feed them through a continuous line that combines pre-treatment, 染色, 洗浄, and sizing. This integrated process reduces handling and eliminates separate re-beaming and sizing stages after dyeing.
This method supports high-volume production and consistent color across large fabric batches. しかし, dye penetration and ring-dye effects vary with process conditions, while uneven yarn tension can cause shade differences across the sheet.
- Market Position: Mass-market and fashion denim that prioritizes volume, delivery speed, and cost control.
- Cost and Efficiency: Integrates multiple stages into one line, reducing handling and labor requirements.
- 柔軟性: Accommodates different shades and production specifications through adjustments to dyeing parameters and line settings.
You may be interested in: ロープ染色とスラッシャー染色の違い
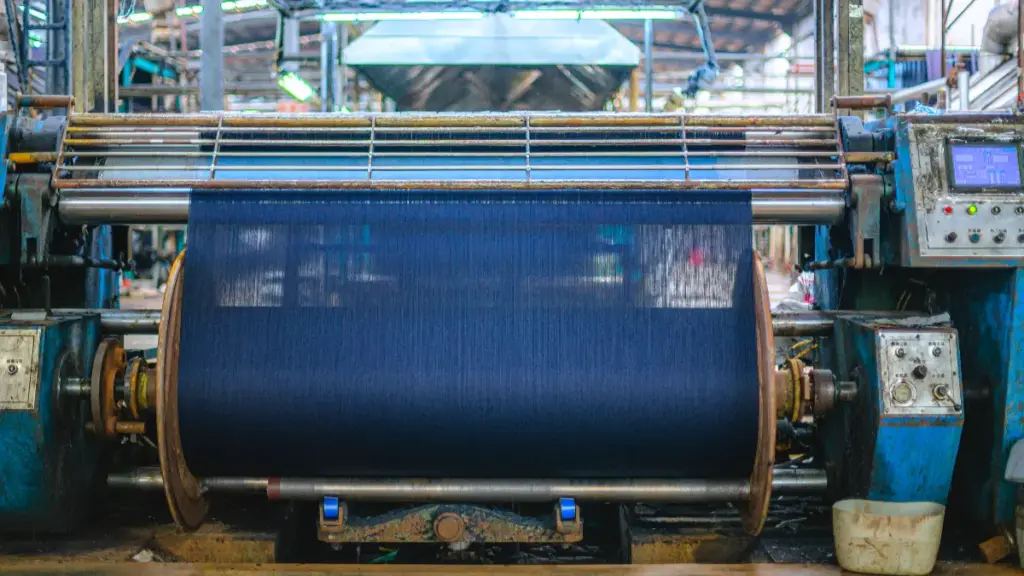
Looking for Consistent Denim Dyeing Quality?
How Denim Manufacturers Control Color Consistency
Consistent denim color requires clear measurement standards and careful process control, helping manufacturers meet buyer specifications and maintain shade consistency across production batches.
Establishing Color Standards and Measurement Protocols
生産が始まる前に, manufacturers and buyers agree on a target shade and acceptable color differences. These standards give quality control teams a clear basis for checking fabric and deciding whether it meets the order requirements.
Mills often use a physical fabric swatch, known as a master shade standard, or digital CIELAB color values to define the target. CIELAB measures color across three dimensions: lightness (L*), red–green (a*), and yellow–blue (b*). A spectrophotometer measures fabric color and calculates the difference (ΔE) between a sample and the approved target.
The acceptable ΔE depends on the buyer’s requirements, 生地, and the measurement conditions. A lower value indicates a closer color match, but manufacturers should follow the agreed tolerance rather than assume one limit suits every denim order.
Manufacturers also need to manage shade variation between fabric rolls. They measure and group rolls by color so cutting teams can use fabric with similar shades for the same garment. This step helps prevent visible differences between panels, especially when a production order includes multiple rolls.
Managing Chemical and Mechanical Dyeing Parameters
Once manufacturers define the color target, they control the dyeing conditions that affect color depth and uniformity. Small changes in dye chemistry, timing, or yarn preparation can produce noticeable differences between batches.
| Parameter | Quality Control Focus |
|---|---|
| Dye Bath Chemistry | Monitor pH and redox potential to maintain suitable conditions for indigo reduction. |
| Dye Concentration | Control dye and chemical dosing to maintain the target shade. |
| Immersion and Oxidation Time | Keep timing consistent across dyeing cycles to control color depth. |
| 糸の準備 | Remove waxes and impurities that may interfere with even dye absorption. |
Automated systems can help mills monitor dye concentration, 温度, and chemical dosing throughout production. Operators also check process records and test samples to identify changes before they affect larger quantities of yarn.
Manufacturers should set operating ranges according to their dyeing equipment, recipe, および生地の要件. Rather than relying on universal pH, redox, or timing values, they should validate the parameters for each process and keep them consistent across production runs. This approach helps reduce shade variation and supports more reliable color matching for bulk denim orders.

Denim Washing Effects After Dyeing Process
Garment washing affects the final color, テクスチャ, and fit of denim jeans. Manufacturers control washing conditions to achieve the required appearance while maintaining fabric quality and dimensional stability.
How Washing Changes Denim Color and Appearance
Garment washing creates different shades and fading patterns by removing loose dye and altering the fabric surface. The choice of wash depends on the desired look, fabric properties, and product specifications.
Common denim washing methods include:
- すすぎ洗い: Removes loose dye and reduces stiffness while preserving a dark, clean appearance.
- ストーンウォッシュ: Uses pumice stones or similar mechanical abrasion to create a worn, uneven fade.
- 酵素ウォッシュ: Uses cellulase enzymes to produce a softer feel and controlled fading.
- 漂白洗浄: Uses bleaching agents to achieve lighter shades and stronger color contrast.
Each method produces different results, so manufacturers need to confirm the wash effect through sample testing before bulk production. They also check color consistency between garments to ensure that the finished jeans match the approved sample.
How Washing Affects Fabric Quality and Fit
Washing changes more than appearance. Mechanical abrasion and chemical treatments can weaken cotton fibers, while removing sizing agents and relaxing the fabric can improve softness and drape. More intensive treatments may cause greater strength loss, so manufacturers need to balance the requested wash effect with durability requirements.
Washing also affects garment dimensions. Fabric relaxation and shrinkage can change the length, waist, and leg measurements of finished jeans. Manufacturers should test shrinkage under the intended washing conditions and check garment measurements against the approved size specifications.
For bulk orders, wash testing and dimensional checks help manufacturers identify potential problems before shipment. By standardizing wash recipes, monitoring processing conditions, and inspecting finished garments, they can maintain more consistent color, 生地の品質, and fit across production batches.
You can learning more about denim washing in: 最高の柔らかさを実現する工業用デニムの洗濯に関する完全ガイド
Quality Testing Standards for Denim Color Performance
Denim’s color durability is not subjective. It’s measured against global AATCC and ISO standards for washing, rubbing, and light exposure, where passing grades are non-negotiable for commercial production.
Core International Test Methods
When brands and mills talk about color performance, they’re referring to a specific set of standardized tests. These aren’t just guidelines; they’re the pass/fail metrics that determine if a fabric lot is commercially viable. The main ones you’ll encounter are from AATCC (American Association of Textile Chemists and Colorists) およびISO (International Organization for Standardization).
- Colorfastness to Washing (AATCC 61, ISO 105-C06): This test simulates how a fabric will react to repeated home laundering. It uses standardized detergents and temperatures to check for two things: how much the original color fades and how much it bleeds onto other fabrics.
- Colorfastness to Rubbing (AATCC 8, ISO 105-X12): Known in the industry as “壊れる,” this test measures how much color transfers from the denim to another surface when rubbed. It’s performed with both a dry and a wet cloth to mimic real-world friction.
- Colorfastness to Light (AATCC 16, ISO 105-B02): This procedure assesses how well the fabric resists fading when exposed to light. It uses a controlled artificial light source that mimics the effects of sunlight over time.
- Colorfastness to Perspiration & 水 (AATCC 15/107, ISO 105-E04/E01): This evaluates how the color holds up against both acidic and alkaline sweat, as well as plain water. It’s crucial for preventing dye from staining a person’s skin or other clothing during wear.
Commercial Performance Grades and Benchmarks
Passing these tests requires meeting specific numerical grades. These grades are the language of quality control between mills and brands. A failure to meet these benchmarks can result in rejected shipments.
- Evaluation Scales: Performance for color change and staining is rated on a standard Gray Scale from Grade 1 (poor) to Grade 5 (excellent). Lightfastness is measured against the 1-8 Blue Wool scale, where a higher number means better fade resistance.
- Washing Fastness Benchmark: For both color change and staining, a passing grade is typically a 3–4 or higher on the 5-point scale. Anything less suggests the color is unstable.
- こする (クロッキング) Benchmark: Most brands demand a Grade 4 for dry rubbing. The real challenge is wet rubbing, where targets are lower, often Grade 2.5–3. This is a known weak point for dark indigo and sulfur-dyed denim.
- Light Fastness Benchmark: For general fashion denim, the fabric usually needs to meet a Blue Wool rating of 4–5. This ensures the garment won’t show significant fading from everyday sun exposure in a retail or wear environment.
Common Denim Dyeing Problems and Solutions
Denim dyeing defects, from uneven color to poor fastness, are fixed by rigorously controlling chemical parameters, mechanical settings, and standardized procedures.
Identifying Common Color and Fabric Defects
Every denim mill runs into the same set of headaches. It’s not a question of if, but when. Knowing what to look for is the first step to diagnosing the root cause instead of just treating symptoms. These are the usual suspects.
- Shading variation: This is the most common one. You get uneven color, including bands that run down the length of the warp or bars (called barré) across the width of the fabric.
- Streaks and marks: These are vertical lines that follow the warp yarns, or they can be compression marks left over from the rope dyeing process itself.
- Batch-to-batch inconsistency: You run the exact same recipe on Monday and again on Wednesday, but you get two different shades. This is a huge problem for any brand that needs consistent product.
- Poor colorfastness: The color rubs off too easily when dry or wet (壊れる), or it fades dramatically after just a few home laundry cycles. This is a quick way to get customer complaints.
- Uneven dye penetration: The indigo sits only on the very surface of the yarn instead of penetrating the core. The color looks weak and abrades away too fast, ruining the intended fade pattern.
- Warp quality issues: This shows up as frequent yarn breaks during dyeing and weaving, along with excessive lint accumulation that can cause secondary defects.
Key Process Controls and Solutions
Fixing these issues isn’t magic. It comes down to disciplined, systematic control over the entire process. You can’t just set it and forget it. If you’re seeing defects, your controls are failing somewhere.
- Chemical parameter control: You must maintain stable pH (typically 11.5–12.5 for indigo), Oxidation-Reduction Potential (ORP), and dye concentration. The best mills use automated sensors and dosing to keep these numbers locked in.
- Mechanical adjustments: Ensure your squeeze rollers apply uniform pressure across their entire width. Keep warp tension systems calibrated and all guide rollers clean and perfectly aligned. A misaligned roller is a guaranteed recipe for streaks.
- Standardized procedures: Use consistent water quality, run strict QC for incoming chemicals, and control your heating and dosing rates. Don’t let operators improvise; every variable must be documented and followed.
- Effective after-washing: A thorough soaping and rinsing process at high temperatures is non-negotiable. It removes unfixed dye from the yarn surface and is critical for achieving good fastness ratings.
- Systematic quality monitoring: Use spectrophotometry to check for shade consistency and keep your color difference (ΔE) 下 1.0. また, run standardized crocking and wash fastness tests on every batch. Data drives decisions.
- Material management: Use a single yarn lot for the weft to prevent barré marks. And perform regular preventive machine maintenance to catch worn parts or alignment issues before they ruin a production run.
Choosing a Denim Manufacturer With Dyeing Expertise
Vetting a mill’s dyeing expertise means digging into their process data and matching their capabilities—rope versus slasher—to your product’s price point and brand positioning.
Evaluating Technical Processes and Quality Control
The first thing to look at is the manufacturer’s primary dyeing method. This choice directly impacts your product’s final look. Rope dyeing is the classic method for premium denim, creating a rich shade and a strong “ring-dye” effect that produces high-contrast fades. スラッシャー染色の方が早い, more integrated process often used for mass-market goods where throughput and cost are the main drivers.
A competent partner must prove they can control their process with hard data. Don’t just take their word for it. They need to show you their systems for managing shade consistency from batch to batch. This isn’t magic; it’s just disciplined manufacturing.
- Shade Consistency: The mill must demonstrate they can hold color tolerance to a Delta E (ΔE) の 1.0 or less against an approved standard. Ask to see their historical control charts.
- Process Control: They need documented operating windows for dye recipes, line speeds, bath pH, 温度, and redox potential. Small deviations here create big problems downstream.
- Defect Prevention: Ask about their quality assurance protocols for catching common defects like streaks, back-staining from unfixed dye, and side-to-center shade variation before the fabric ever gets to you.
Matching Capabilities to Your Product Strategy
Technical skill is only half the equation. The manufacturer’s operational model must align with your business needs. 例えば, rope dyeing is often slower and requires more setup than high-volume slasher dyeing. You need to align their capacity and lead times with your production calendar and order sizes.
サステナビリティはもはやオプションではありません. A serious dyeing partner will be able to provide data on their water consumption per meter and their chemical management practices. Ask for their certifications, like GOTS, エコテックス, またはブルーサイン, and verify they are current. This is a direct reflection of their operational discipline and long-term viability.
結局のところ, the choice has to fit your product strategy. If you’re making a premium, raw denim jean designed for heritage fades, a mill with rope dyeing expertise is the right fit. If you’re producing a high-volume, price-sensitive fashion item, a slasher-focused mill makes more sense. The manufacturer’s capabilities must match your product’s price point, performance requirements, and what your brand stands for in the market.
最終的な考え
Denim dyeing methods, including rope dyeing and slasher dyeing, affect color depth, yarn characteristics, 生産効率, and the appearance of finished jeans. Consistent results depend on controlling dyeing parameters, checking shade variations, and testing fabric performance under the intended washing conditions. These quality control measures help denim manufacturers meet brand specifications and maintain consistency across production batches.
チャンゴン supports denim brands with manufacturing expertise and quality control throughout production. チャンホンに連絡する to discuss your denim requirements and request fabric samples to evaluate color, テクスチャ, and performance before placing a bulk order.
よくある質問
How are jeans dyed?
Jeans get their color at the yarn stage, before the fabric is even woven. Mills dye the warp (縦方向に) yarns using indigo in a process that creates a ‘ring-dye’ 効果, where the color sits on the outside of the yarn, leaving the core white. These blue warp yarns are then woven with white weft (crosswise) yarns to create denim. After the jeans are sewn, they often go through washing and finishing processes that start to wear away the surface dye, creating fades.
What dye is used for denim?
Indigo is the classic and most common dye used for blue jeans. Most modern production uses a synthetic version of indigo because of its consistency and cost. Sulfur dyes are also widely used, especially for making black, グレー, and other colored jeans. Sometimes, mills combine both indigo and sulfur dyes to create unique deep blue or blue-black shades.
Why does denim fade after washing?
Denim fades because of how the warp yarns are dyed. The indigo color only coats the surface of the yarn, leaving the inner core white. This is called ‘ring-dyeing’. When you wash and wear your jeans, the friction and agitation rub away the outer layer of dye, slowly exposing the white core underneath. This is what creates the unique fading patterns.
How do manufacturers make dark blue jeans?
To get a deep, dark blue color, manufacturers increase the number of times the cotton yarn is dipped into the indigo dye. A typical pair of jeans might get 6-8 dips, but a dark pair could get 12 以上. Each dip adds another thin layer of color. Mills also might add sulfur dyes on top of or underneath the indigo layers to make the shade even deeper and achieve blue-black or near-black tones.
What is the indigo dyeing process?
Indigo dyeing is a multi-step process. Since indigo doesn’t dissolve in water, it first has to be chemically changed into a soluble, yellowish-green form. Cotton yarns are dipped into this solution. それから, the yarns are pulled out and exposed to air. The oxygen in the air turns the dye back into its insoluble blue state, fixing it onto the surface of the fibers. This dip-and-oxidize cycle is repeated multiple times to build up the final color.
How do brands control denim color consistency?
Brands use a combination of strict process controls, テクノロジー, and standards. 染色中, mills monitor and control factors like dye concentration, pH, 温度, and line speed. They use spectrophotometers to measure color numerically, ensuring each batch matches an approved standard within a tight tolerance (often less than 1.0 ΔE). Fabric rolls are often sorted into shade bands, and brands approve lab dips and pilot washes before starting full production to ensure the final garment looks exactly as intended.